
Blog
Cummins ISX & QSX Wet Cylinder Liner Installation & Protrusion Steps
Precision cylinder liner seating and 4-quadrant protrusion measurement guidelines for commercial Cummins rebuilders.
Installing new flat-top or grooved-top wet cylinder liners during an in-frame overhaul on a Cummins ISX15 or QSX15 engine? Follow this step-by-step professional workshop procedure to clean block counterbore ledges, lubricate lower O-rings, seat liners concentrically with the 16.00-pound M20167-A Liner Press, and verify 4-quadrant liner protrusion.
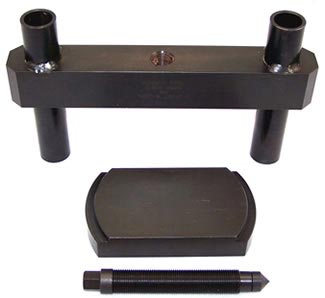
Why Wooden Blocks & Dead-Blow Hammers Ruin ISX/QSX O-Rings & Head Gaskets
On Cummins ISX and QSX heavy-duty diesel engines, wet cylinder liners are sealed at the bottom by tight-fitting elastomer packing rings that require firm, uniform vertical pressure to enter the lower block bore without rolling or shearing. Technicians who attempt to drive new ISX liners home using a 2x4 block of wood and a dead-blow hammer create uneven side loads—pinching lower O-rings (leading to immediate coolant-in-oil leaks) or chipping delicate grooved-top anti-polishing steps. Worse, incomplete flange seating produces false liner protrusion readings that guarantee premature head gasket failure. Utilizing the 16.00-pound M20167-A Liner Press Kit (Cummins 3164606 / 3162461 / 3164607 Equivalent) eliminates every installation risk by applying smooth, centered mechanical press force straight down the cylinder axis.
The 5-Step Cummins ISX & QSX Liner Installation & Protrusion Protocol
- Clean Block Counterbore Ledge & Lower O-Ring Bores: Thoroughly clean the upper cylinder block counterbore seat and lower packing-ring bores until 100% free of rust, scale, and old sealant; inspect counterbore depth and flatness prior to liner insertion.
- Install & Lubricate Liner O-Rings / Crevice Seals: Install fresh OEM packing rings onto the new flat-top or grooved-top ISX/QSX cylinder liner without twisting, and apply clean vegetable oil or Cummins-approved assembly lubricant evenly to the O-rings and lower block bore.
- Start Liner Squarely & Mount M20167-A Liner Press Fixture: Lower the cylinder liner gently into the block bore until the lower O-rings rest at the lower bore chamfer, then position the M20167-A press plate squarely on top of the liner and bolt the bridge assembly to the cylinder block head-bolt holes.
- Advance Forcing Screw Smoothly to Seat Liner Flange Flush: Lubricate the M20167-A forcing screw threads and turn clockwise smoothly with a hand wrench until the liner enters the lower bore and seats firmly against the upper block counterbore ledge.
- Measure 4-Quadrant Liner Protrusion with Dial Indicator: Remove the M20167-A press (or measure with a liner hold-down clamp per Cummins manual) and check liner flange protrusion at 12, 3, 6, and 9 o'clock positions using a calibrated dial depth gauge to confirm specs before installing the cylinder head.
PRO-TECH O-RING LUBRICATION & ANTI-POLISHING GROOVE MANDATE:
NEVER PRESS CUMMINS ISX/QSX LINERS IN DRY OR USE PETROLEUM GREASE THAT SWELLS SILICONE/EPDM RINGS! Always use Cummins-approved O-ring lubricant so lower packing rings slide cleanly without rolling or pinching! ON GROOVED-TOP LINERS, ensure the M20167-A press plate sits squarely without pinching the anti-polishing ring step!
16.00 lbs Heavy-Duty Cummins ISX / QSX Flat-Top & Grooved-Top Liner Press Kit. Guarantee Exact Protrusion.
Get the M20167-A Liner Press Now
overall rating:
my rating:
log in to rate