
Blog
Cummins NT & N14 Cylinder Liner Service Steps
Precision engine rebuilding and wet cylinder liner service guidelines for commercial diesel mechanics and machine shop technicians.
Removing or installing 5.5-inch bore wet cylinder liners on Cummins NT 855 or N14 engines during an in-frame or complete overhaul? Follow this step-by-step professional workshop procedure to extract stuck liners with the M20105 puller, clean block bore lands, lubricate new O-rings, configure the press assembly, and seat liners flush without O-ring damage or protrusion errors.
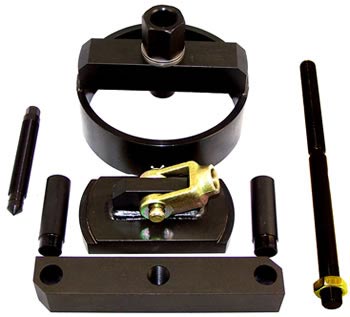
Why Impact Driving & Freehand Pulling Destroy Cummins Engine Blocks
On Cummins NT and N14 engines, cylinder liner installation is a precision operation that dictates engine longevity. Lower liner seals consist of rubber D-rings and Crevice Seals that expand against lower block bore lands to hold back high-pressure coolant. When technicians attempt to drive new liners into place using sledgehammers or heavy drivers, the impact force cocks the liner. The sharp lower edge of a cocked liner acts like a knife, shearing or twisting the rubber seals against the block chamfer. Sliced seals result in immediate coolant leaks into engine oil upon refilling the radiator, requiring an immediate teardown. During removal, prying stuck liners with pry bars or slide hammers gouges the cast-iron sealing lands, permanently damaging the engine block. Utilizing the 24-pound M20105 Puller & Press Combo completely eliminates installation and extraction hazards. The tool applies smooth, linear mechanical pressure, extracting old liners straight up and pressing new liners straight down to guarantee 100% O-ring preservation and exact counterbore seating.
The 5-Step Cummins NT/N14 Liner Service Protocol
- Configure M20105 for Liner Extraction (Puller Mode): Assemble the M20105 puller feet underneath the bottom rim of the target 5.5" liner. Seat the heavy bridge plate squarely on the block deck face.
- Extract Old Cylinder Liner Smoothly: Lubricate forcing screw threads with engine oil. Turn the forcing nut clockwise with a hand wrench to draw the stuck liner straight up out of the block without scoring bore lands.
- Clean Block Lands & Prep New 5.5" Liner: Thoroughly wire-brush and clean rust, scale, and old seal residue from lower block lands and upper counterbores. Install new Crevice Seals and D-rings onto the new Cummins liner, coating seals with approved vegetable oil lube.
- Configure M20105 for Liner Pressing (Press Mode): Slide the new liner squarely into the block bore. Place the M20105 press plate over the top rim of the liner and anchor the puller rod to the block deck per tooling instructions.
- Press Liner Dead-Flat & Verify Protrusion: Turn the forcing screw to press the liner down smoothly past lower chamfers until the upper flange sits flush on the counterbore ledge. Measure final liner protrusion across four quadrants with a dial depth gauge to verify OEM specification.
PRO-TECH O-RING LUBRICATION & HAND WRENCH MANDATE:
ALWAYS USE APPROVED O-RING LUBE (VEGETABLE OIL SOAP) ON NEW SEALS! Petroleum grease WILL swell and destroy rubber Crevice Seals! ALWAYS TURN FORCING SCREWS WITH A HAND WRENCH OR RATCHET—never spin forcing screws with heavy air impact guns during liner press operations!
24.00 lbs Precision 5.5" Bore Cylinder Liner Puller & Press System. Protect Cummins Overhauls.
Get the M20105 Combo Tool Now
overall rating:
my rating:
log in to rate