
Blog
Cummins ISX & X15 Head Bolt & Main Cap Torque Steps
Precision engine fastener mechanics and torque-angle guidelines for commercial diesel mechanics and fleet rebuilders.
Installing cylinder head bolts or main bearing cap fasteners on a Cummins ISX or X15 engine during an in-frame repair or complete overhaul? Follow this step-by-step professional workshop procedure to clean fastener threads, lubricate bolt flanges, seat the ATC24MMISX-A 24mm socket, perform multi-step torque sequences, and use the laser-etched 90° marks to execute accurate angular turns without rounding bolt heads.
Why Standard Sockets Cause Main Bearing Cap Walk & Head Gasket Blowouts
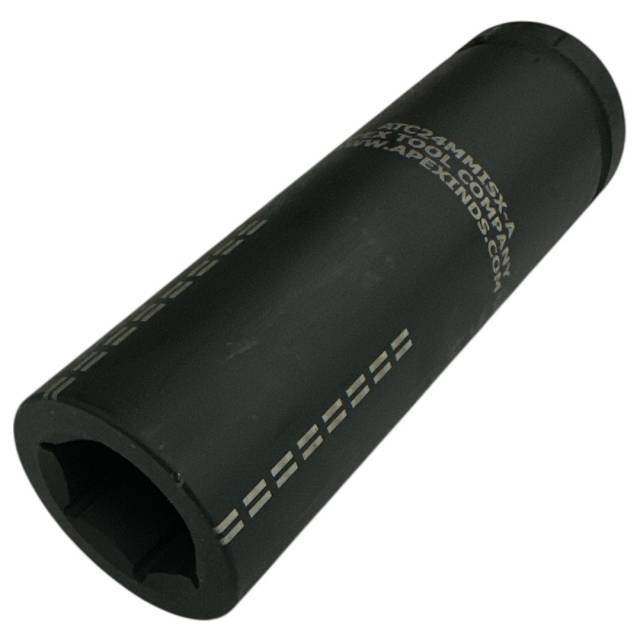
On Cummins ISX and X15 heavy-duty engines, cylinder head bolts and main bearing cap bolts must withstand immense cylinder pressures and torsional crankshaft loads. Cummins utilizes a strict Torque-Plus-Angle tightening specification for these 24mm fasteners to guarantee consistent bolt stretch across the engine block. Technicians who attempt this critical process using generic 1/2" drive impact sockets or 12-point chrome sockets encounter severe mechanical problems. Standard 1/2" drive extensions flex under extreme foot-pound loads, absorbing rotational energy so the bolt shank receives less turn than the wrench handle indicates. This results in under-torqued main caps that suffer "main cap walk"—a condition where the bearing cap micro-shifts under load, destroying main bearings and scoring the crankshaft journals. Furthermore, 12-point sockets contact only the extreme corners of 24mm bolt heads, slipping under high torque and rounding the bolt flats. Rounded head bolts stall engine rebuilds and require burning or drilling out hardened steel fasteners inside the block deck. Utilizing the 2.00-pound ATC24MMISX-A 24mm ¾" Drive Socket eliminates these risks completely. Its heavy-wall 6-point design grips fastener flats securely, while its 5-inch solid length transfers 100% of torque force directly to the bolt shank.
The 5-Step Cummins ISX/X15 Torque-Angle Fastener Protocol
- Clean & Inspect Fastener Holes & Threads: Chase engine block deck threads with a thread tap. Clean out oil sludge and debris from blind holes using compressed air. Inspect 24mm bolt threads and under-head flanges for distortion.
- Lubricate Threads & Bolt Head Contact Surfaces: Apply clean engine oil or specified Cummins thread lubricant to bolt threads and under-head seating flanges per factory service manual instructions.
- Execute Initial Base Torque Sequence with ATC24MMISX-A: Attach the ATC24MMISX-A socket to a calibrated ¾" drive torque wrench. Torque all 24mm head bolts or main cap bolts in the prescribed factory crisscross pattern to the initial base foot-pound specification.
- Align Laser-Etched 90° Marks & Perform Angle Rotation: Align the laser-etched 90-degree index line on the ATC24MMISX-A socket with a static reference point on the engine block or cam box. Pull the breaker bar in a smooth, continuous motion until the socket rotates exactly 90 degrees to the secondary mark.
- Final Inspection & Pattern Verification: Mark each torqued bolt head with a paint pen to confirm completion. Verify that all fasteners have received the full specified angular turn before installing cam boxes, oil pans, or valve train components.
PRO-TECH THREAD CLEANING & CONTINUOUS ANGLE PULL MANDATE:
ALWAYS BLOW OUT BLIND THREAD HOLES! Trapped oil or coolant in bolt holes WILL hydro-lock and crack cast-iron engine blocks during bolt insertion! ALWAYS EXECUTE ANGLE TURNS IN ONE SMOOTH, CONTINUOUS PULL! Stopping mid-turn introduces friction resistance that distorts final stretch values!
2.00 lbs Precision 24mm ¾" Drive 5" Extended Torque-Angle Socket. Protect Cummins Overhauls.
Get the ATC24MMISX-A Socket Now
overall rating:
my rating:
log in to rate