
Blog
Cummins C Series & ISL/ISC Counterbore Resurfacing Steps
Precision engine block machining and deck reconditioning guidelines for commercial diesel mechanics and machine shops.
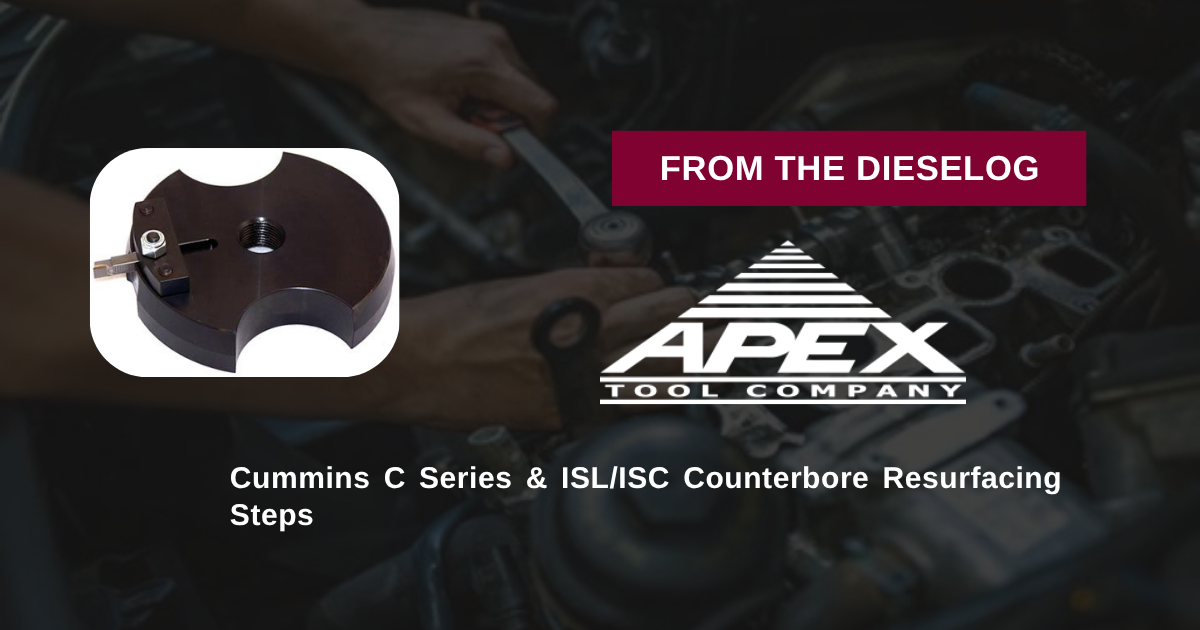
Resurfacing upper cylinder liner counterbores on Cummins C8.3, C8.9, ISL, or ISC engine blocks during an in-frame repair or complete overhaul? Follow this step-by-step professional workshop procedure to set up the M20162 cutter plate, align the M50134 cutter drive assembly, execute precision cutting passes, measure counterbore depth, and select stainless steel shims cleanly.

Why "Improvised" Alignment Guides Ruin Heavy-Duty Cummins Engine Blocks
On Cummins C Series and ISL/ISC engines, maintaining exact cylinder liner protrusion is essential for long-term head gasket retention and cylinder sealing. When fretting or carbon erosion damages the counterbore ledge, machining a fresh, flat seat is required before installing counterbore shims. However, attempting to machine this seat without a dedicated cutter plate like the M20162 introduces catastrophic errors. Using unguided or non-specific cutter plates allows the drive shaft to wobble off-center. This orbital wobble cuts an oval or tapered ledge instead of a flat ring. When a counterbore shim is placed over a tapered ledge, it bends under cylinder head torque, concentrating high stress on one side of the cylinder liner flange. This uneven loading cracks the liner flange or causes the liner to drop under load, resulting in immediate head gasket failure and severe coolant contamination in the oil crankcase. Utilizing the 7.00-pound M20162 Counterbore Shim Cutter Plate completely eliminates alignment errors. Its application-specific guide pilots squarely into Cummins C8.3, C8.9, ISL, and ISC cylinder bores, locking the M50134 drive assembly perpendicular to the deck face to deliver dead-flat, mirror-smooth counterbore seats every time.
The 5-Step Cummins Counterbore Resurfacing & Shim Preparation Protocol
- Clean Engine Block Deck & Inspect Counterbore Bores: Remove old cylinder liners. Clean internal counterbore ledges thoroughly with solvent and a wire brush to remove rust, carbon, and old gasket residue.
- Mount M20162 Cutter Plate onto Block Deck: Position the M20162 cutter plate squarely into the target cylinder bore. Ensure the plate seats flush against the block deck, anchoring it securely per tooling instructions.
- Assemble M50134 Drive Unit & Set Cutting Bit Depth: Insert the M50134 counterbore drive tool through the center pilot of the M20162 plate. Set the carbide cutter bit to contact the highest point of the damaged counterbore ledge.
- Execute Smooth Machining Passes to Clean Ledge: Turn the cutter drive handle smoothly while applying steady, light downward feed pressure. Advance the bit incrementally until the counterbore seat is completely resurfaced and free of pitting or corrosion.
- Clean Shavings, Measure Depth & Select Stainless Shims: Vacuum iron filings out of the cylinder bore. Measure the newly machined counterbore depth using a depth micrometer or sled gauge. Select the correct thickness Cummins stainless steel counterbore shim to achieve exact factory liner protrusion specifications.
PRO-TECH CHIP EVACUATION & FEED PRESSURE MANDATE:
VACUUM CAST IRON SHAVINGS FREQUENTLY DURING CUTTING! Trapped filings under the cutter bit WILL cause chatter ridges and uneven seat depths! ALWAYS APPLY UNIFORM, LIGHT FEED PRESSURE—never force or slam the cutter tool onto the cast-iron ledge!
7.00 lbs Precision Counterbore Shim Cutter Plate. Protect Cummins Engine Rebuilds.
Get the M20162 Plate Now
overall rating:
my rating:
log in to rate