
Blog
CAT 3176, 3300 & 3406 Counterbore Boring Steps
Precision engine block machining and deck reconditioning guidelines for commercial diesel mechanics and machine shops.
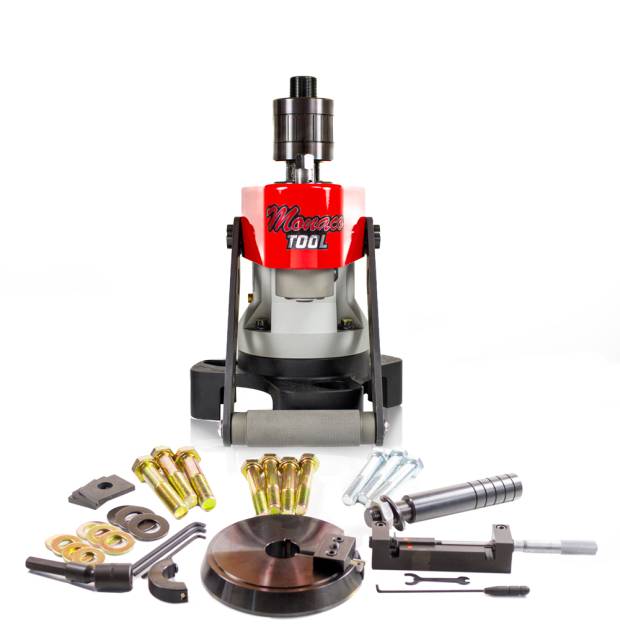
Resurfacing upper cylinder liner counterbore ledges on a Caterpillar 3176, 3306, 3406, or C15 engine block during an in-frame overhaul? Follow this step-by-step professional workshop procedure to clean block decks, anchor the 3-legged M52051 boring assembly, utilize the removable handle in tight bays, set micro-fine depth passes, machine dead-flat ledges, and select counterbore shims cleanly.
Why 2-Legged Tools & Handheld Cutters Fail on Hardened Cast Iron
On Caterpillar heavy-duty engines, cylinder liner protrusion must be precise and uniform across all cylinders to guarantee proper head gasket retention. When counterbore ledges suffer erosion or fretting, machining a fresh, flat surface is required before installing counterbore shims. However, attempting to machine these ledges using 2-legged puller-style cutters or handheld rotary tools causes severe block damage. A 2-legged tool lacks geometric stability; as turning force is applied, the spindle flexes off-axis, cutting an oval or tapered ledge. When a counterbore shim is placed on a tapered ledge, the cylinder liner cocks under head bolt torque, concentrating extreme stress on one side of the liner flange. This uneven loading cracks the liner flange or causes the liner to drop under load, resulting in immediate head gasket failure and severe coolant contamination in the oil pan. Utilizing the 91-pound M52051 3-Legged Counterbore Boring Tool (PT-7025 / 9U-7990 Equivalent) eliminates alignment defects completely. Its heavy 3-point tripod base bolts firmly to the block deck, locking the spindle 100% perpendicular to deliver dead-flat, mirror-smooth counterbore seats every time.
The 5-Step CAT Counterbore Boring & Machining Protocol
- Clean Block Deck & Inspect Bore Ledges: Remove old cylinder liners. Stone the engine block deck face flat and clean counterbore ledges thoroughly with solvent and a wire brush to remove rust, carbon, and old gasket residue.
- Mount & Anchor M52051 3-Legged Base to Block: Position the M52051 3-legged base squarely over the target cylinder. Anchor the tripod legs securely into adjacent head bolt holes per tooling instructions, verifying absolute deck flushness.
- Install Adapter Head & Set Bit Depth: Attach the application-specific cutter head and adapter. Advance the carbide bit until it contacts the highest point of the damaged counterbore ledge, then set the micro-adjuster depth ring to target depth.
- Execute Smooth Machining Passes (Utilize Removable Handle): Attach the drive handle (or remove it for clearance under tight firewalls). Turn the spindle smoothly while applying steady, light downward feed pressure. Advance the bit incrementally until the ledge is 100% resurfaced and chatter-free.
- Vacuum Filings, Measure Depth & Select Stainless Shims: Vacuum cast-iron shavings out of the bore. Measure the newly machined counterbore depth using a depth micrometer or sled gauge across four quadrants. Select the correct thickness Caterpillar stainless steel counterbore shim to achieve exact factory liner protrusion.
PRO-TECH VACUUM FILINGS & LIGHT DOWNWARD FEED MANDATE:
VACUUM CAST IRON SHAVINGS FREQUENTLY DURING CUTTING! Trapped filings under the carbide bit WILL cause chatter ridges and uneven seat depths! ALWAYS APPLY UNIFORM, LIGHT DOWNWARD FEED PRESSURE—never force or slam the cutter spindle onto the cast-iron ledge!
91.00 lbs Made-in-USA 3-Legged Counterbore Boring Machine. Protect CAT Overhauls.
Get the M52051 Tool Now
overall rating:
my rating:
log in to rate