
Blog
Cummins Big Cam, Small Cam & N14 Camshaft Bearing Replacement Steps
Precision engine block maintenance guidelines for heavy diesel rebuilders and machine shop mechanics.
Replacing worn camshaft bearings during a major engine overhaul on a Cummins Big Cam, Small Cam, or N14 diesel engine? Follow this step-by-step professional workshop procedure to set up the M20060 55-inch drive bar, expand guide collets into adjacent block webs, align oil feed holes, and pull or drive bearings smoothly into position.
Why Improvised Universal Drivers Cause Fatal Cam Journal Seizures
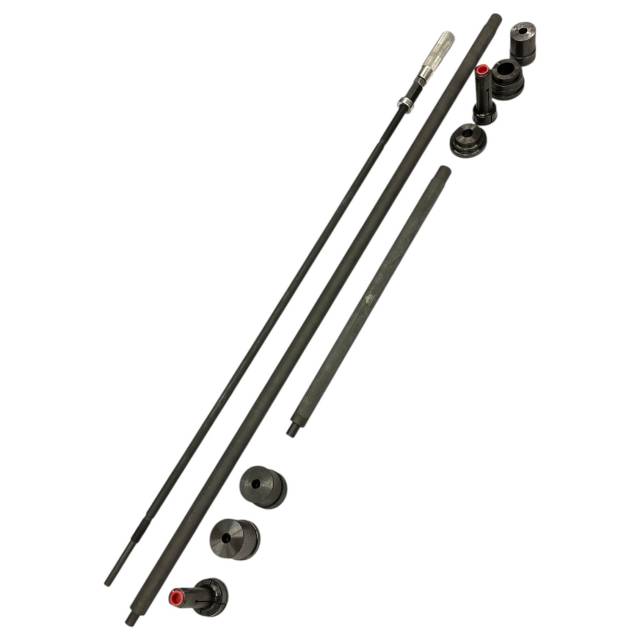
On Cummins N14, Big Cam, and Small Cam heavy-duty engines, camshaft bearings operate in narrow housing bores located deep inside the crankcase structure. Because these engines utilize high valve spring pressures and unit injector pushrod loads, the camshaft journals require uninterrupted oil flow through tiny oil feed passages in the block webs. Technicians who attempt to replace cam bearings using universal split-sleeve drivers or short hammers run into major failure points. Short tools cannot maintain perpendicular alignment across 5 feet of engine block length, causing the driver head to tilt. Driving a tilted bearing gouges deep scratches into the aluminum or cast-iron block bore, creating permanent oil pressure leaks around the bearing outer diameter. Even worse, if the bearing is driven past its designated depth without a guided stop, the oil feed hole is covered, causing total oil starvation. The resulting journal seizure destroys the camshaft and ruins the entire engine block. Utilizing the 61-pound M20060 Master Cam Bearing Kit eliminates these service failures completely. By feeding the 55-inch precision drive bar through multiple centering collets in adjacent block webs, the tool maintains perfect 360-degree concentricity, driving or pulling bearings dead-straight into position with exact oil passage indexing.
The 5-Step Cummins Cam Bearing Service Protocol
- Clean & Inspect Engine Block Cam Housing Bores: Remove old camshaft bearings using the M20060 puller assembly. Clean all internal block web housing bores thoroughly using solvent and fine Scotch-Brite. *Verify oil feed holes in the block webs are 100% clean and clear of carbon or metal debris.*
- Assemble Drive Bar & Position Centering Collets: Feed the 55-inch M20060 drive bar through the engine block. Insert the expanding centering collets into adjacent block webs and tighten them to lock the drive bar dead-center along the camshaft tunnel axis.
- Select Stepped Adapter & Align Bearing Oil Passages: Mount the correct stepped bearing adapter onto the drive bar. Slide the fresh camshaft bearing onto the adapter. *CRITICAL: Align the oil feed holes in the fresh bearing perfectly with the oil gallery holes in the engine block web before driving!*
- Drive or Pull Bearing into Block Web: Apply clean engine assembly lube to the outer bearing surface and bore chamfer. Using a heavy brass mallet on the drive bar cap or turning the mechanical forcing nut, advance the bearing smoothly into the block web until it reaches its exact depth stop.
- Verify Oil Hole Alignment & Measure Journal Clearance: Remove the M20060 tool assembly. Using a bore scope or mirror, visually verify that the bearing oil hole matches the block gallery 100%. Measure internal bearing ID with a telescoping gauge to confirm zero shell distortion before sliding in the camshaft.
PRO-TECH OIL HOLE ALIGNMENT & ISX COMPATIBILITY WARNING:
ALWAYS VISUALLY VERIFY OIL HOLE ALIGNMENT before driving the bearing to final depth! A covered oil hole WILL seize the camshaft on initial startup! NOTE: THIS KIT IS DESIGNED SPECIFICALLY FOR CUMMINS BIG CAM, SMALL CAM, NH, NT, AND N14 ENGINES ONLY; IT DOES NOT FIT CUMMINS ISX ENGINES!
61 lbs Solid Structural Steel Master Driver & Puller Assembly. Protect Cummins Overhauls.
Get the M20060 Master Kit Now
overall rating:
my rating:
log in to rate