
Blog
Cummins N14 & NT855 Rear Main Seal & Wear Sleeve Installation Steps
Precision rear-end maintenance guidelines for commercial fleet and Class 8 mechanics.
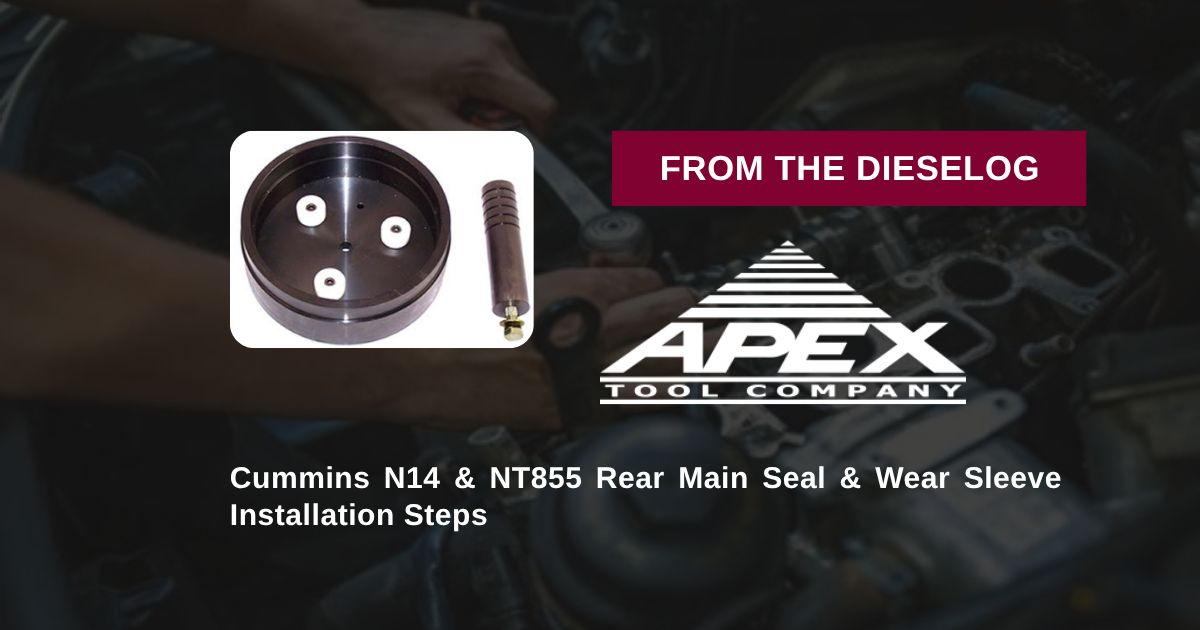
Renewing a grooved rear crankshaft flange and installing a new rear main oil seal during an overhaul or clutch replacement on a Cummins N14, NT855, or NH engine? Follow this step-by-step professional workshop procedure to set up the M20109-A driver assembly, locate the seal retainer plate, press the wear sleeve smoothly, and seat the seal to exact OEM depth.

Why Off-Center Impact Distorts N14 Wear Sleeves & Destroys Clutch Packs
On Cummins N14 and NT855 14-liter commercial engines, the rear crankshaft main seal isolates high oil pressures from the clutch housing. When replacing a worn seal, technicians frequently encounter a deep wear groove carved into the steel crankshaft flange. Installing a replacement rear wear sleeve restores a pristine sealing surface, but the thin stainless steel sleeve requires 100% parallel force to seat without distortion. When mechanics attempt to drive the wear sleeve or rear seal using hammers or brass drifts, uneven impact cocks the sleeve on the flange entrance chamfer. Pushing a cocked sleeve stretches the metal wall, creating microscopic waves along the sealing contact zone. When the rear main seal is installed over a wavy sleeve, oil instantly scours past the sealing lip upon engine startup, slinging crankcase oil across the flywheel and destroying expensive clutch friction discs. Utilizing the 16-pound M20109-A driver tool eliminates these installation failures entirely. Designed with an inner pilot that aligns directly over the crankshaft nose, the tool engages the retainer plate and distributes dead-blow driving force 360 degrees around the perimeter, sliding both the sleeve and seal on squarely until the driver bottoms firmly against the factory shoulder stop.
The 5-Step Cummins N14 Rear Seal & Wear Sleeve Installation Protocol
- Clean & Inspect Crankshaft Flange & Retainer Plate: Remove the flywheel and old rear seal. Clean the crankshaft flange and retainer plate bore thoroughly using solvent and fine Scotch-Brite to remove oil sludge, rust scale, and burrs. *Inspect the flange chamfer for sharp edges before proceeding.*
- Apply Retaining Compound to Crankshaft Flange: Apply a light, uniform film of high-temperature anaerobic retaining compound (such as Loctite 609) to the crankshaft flange OD to prevent oil migration underneath the wear sleeve inner diameter.
- Position Wear Sleeve, Seal & M20109-A Driver: Position the fresh wear sleeve and rear main oil seal over the crankshaft flange entrance. Mount the M20109-A driver cup over the components, ensuring the inner pilot engages the crankshaft nose and aligns squarely with the retainer plate.
- Drive Components to Depth Stop with Dead-Blow Mallet: Using a heavy brass or dead-blow mallet, strike the center anvil face of the M20109-A driver squarely. Advance the driver until the tool shoulder bottoms out flush against the retainer plate face. *Listen for the solid metallic tone indicating full depth seating.*
- Remove Tool & Inspect Installed Components: Pull the M20109-A driver assembly off the crankshaft. Wipe away excess retaining compound. Inspect the wear sleeve and seal 360 degrees to verify both are seated perfectly square, flat, and un-distorted with zero lip rollover. Reinstall the flywheel and torque bolts to Cummins OEM manual specifications.
PRO-TECH RETAINING COMPOUND & DEAD-BLOW MALLET MANDATE:
ALWAYS APPLY ANAEROBIC RETAINING COMPOUND to prevent oil weeping underneath the wear sleeve ID! ALWAYS strike the M20109-A driver using a heavy DEAD-BLOW MALLET or brass hammer squarely on the central anvil face—never use steel sledgehammers that could mushroom the tool collar!
16 lbs Precision Structural Tool Steel Dual-Function Kit. Protect Cummins N14 Overhauls.
Get the M20109-A Service Tool Now
overall rating:
my rating:
log in to rate